Severe wall sticking in a disc granulator doesn’t necessarily mean the formula needs changing. Raw material moisture content exceeding 35%, peeling of the anti-stick coating on the inner wall of the disc, or scraper failure can all cause wall sticking. Checking moisture content and scrapers first, and then considering formula adjustments, is a more efficient troubleshooting approach. The essence of wall sticking is that the adhesion between the material and the disc surface exceeds the dynamic balance between centrifugal force and scraper cleaning force. First, distinguish whether it’s “the material is too sticky” or “the cleaning is inadequate” to address the problem effectively.
I. Comparison of Wall Sticking Locations and Causes
A large area of hard crust forming on the bottom of the disc is often seen when the moisture content of the incoming material is high (exceeding 35%). The material is compacted while at the bottom of the disc, and after the moisture evaporates, a hard layer forms. Material accumulation at the angle between the disc edge and the bottom is usually due to worn bottom scrapers or excessively large gaps, preventing scraping of the dead corners, allowing wet material to slowly accumulate and dry. A sheet-like adhesion on the upper part of the disc wall is often related to the partial detachment of the anti-stick coating or liner, with exposed metal or rough surfaces providing adhesion points for the wet material. If the entire disc surface is uniformly covered with a layer of wet material, it suggests that the material itself is too sticky (e.g., high-starch, high-sugar raw materials), or that the rotation speed is too low, causing the material to remain on the disc surface for too long.
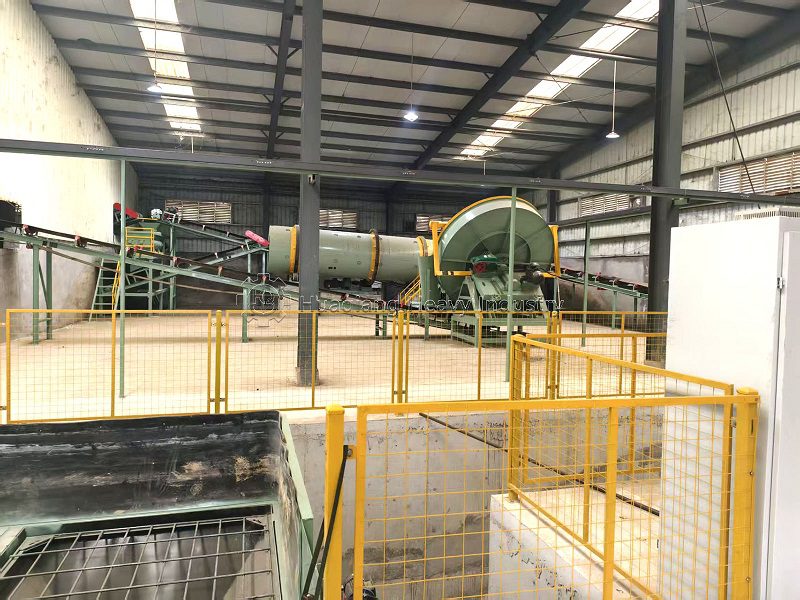
II. Troubleshooting Sequence for Scraper, Coating, and Moisture
Step 1: Check Moisture Content. Use a rapid moisture meter to measure the moisture content of the material entering the disc. The suitable moisture content for organic fertilizer disc granulation is usually between 25% and 35%. Above 35%, the risk of adhesion to the wall increases sharply; below 25%, nucleation is difficult. On-site judgment: It is suitable if it can be formed into a clump when grasped by hand but easily dispersed upon light touch; if water drips from between fingers but does not disperse when dropped, it is too wet and needs to be mixed with dry material or dried.
Step 2: Check the Scraper. The scraper is a core, easily damaged component of the anti-stick coating. Check if the scraper head wear exceeds 3 mm, if the installation angle deviates from 15°–20°, and if the gap between the scraper and the bottom of the disc falls within the 5–10 mm range. Fixed scrapers can only scrape the surface. If a hardened material layer has already formed on the disc, consider upgrading to a spring-loaded or reciprocating scraper, which can improve cleaning efficiency several times over.
The third step is to check the coating or liner. If the polyethylene, polypropylene, or Teflon liner on the bottom and edges of the disc partially detaches, that area will become the first point of adhesion. A modular liner design allows for easy replacement of individual pieces, eliminating the need to replace the entire disc.
If all three are normal, then review the formulation to see if the proportion of high-viscosity raw materials needs to be reduced.
III. Process Countermeasures for High-Viscosity Materials
If the inherent viscosity of the raw material cannot be avoided, it’s better to address it from the process side than to rely on the equipment. Adding aggregate to reduce viscosity is the preferred method: add straw powder, fly ash, or dry recycled material at a ratio of 10%–30%. This reduces moisture content and creates a frictional skeleton within the material, allowing it to “roll” rather than “stick.” Parameter matching is equally crucial: For sticky materials, appropriately increase the tilt angle (e.g., 45°–55°) and rotation speed to shorten the contact time between the material and the disc surface, using centrifugal force to assist in detachment. In terms of formulation, some bentonite can be replaced with a composite system of calcium lignosulfonate and potassium humate to reduce material adhesion while maintaining pellet formation.
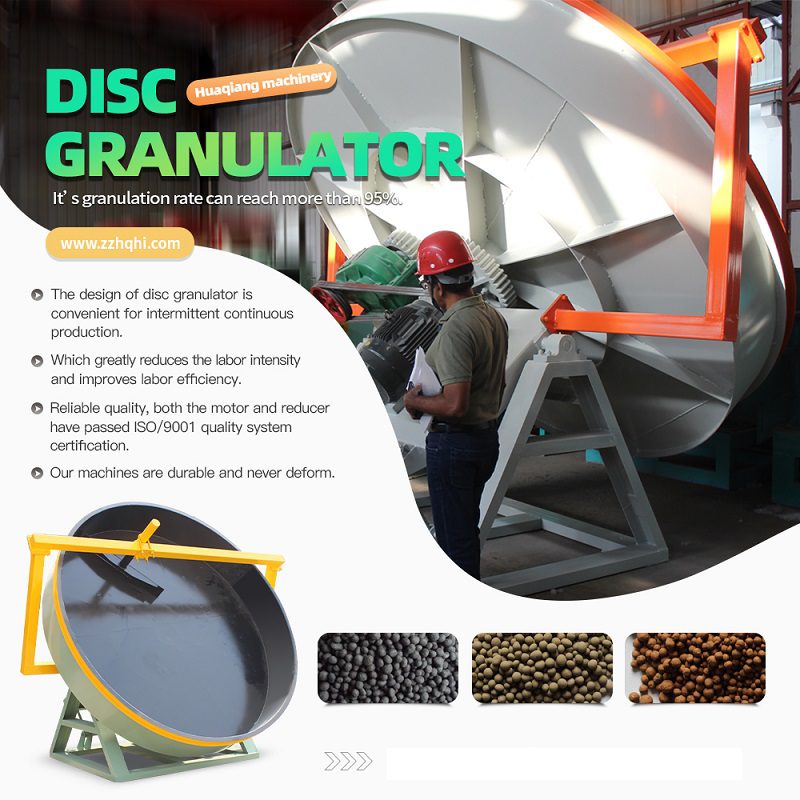
IV. FAQ: Will the material lumps that stick to the disc block the discharge port?
Q: Will the dry, hard material lumps that fall from the disc wall into the finished product block the subsequent discharge port or screen?
Yes, and this is a more insidious risk than “reduced pellet formation rate” in the problem of sticking to the disc. The detached material lumps are often much larger than normal particles. After entering the screening machine, they will get stuck in the screen holes or accumulate at the corners of the discharge chute, causing a decrease in screening efficiency or even blockage and shutdown. More problematic is that if these lumps mix into the finished product, they will damage particle uniformity and become a new source of pulverization during packaging and transportation. The solution isn’t to wait for it to fall and then pick it up. Instead, assuming the scraper and liner are functioning properly, add a grid or coarse screen at the discharge port or before screening to intercept it. Simultaneously, control the wall adhesion to a state where “a thin layer is scraped off,” preventing material lumps from growing to a thickness that allows them to detach completely.
For disc granulators, wall adhesion is often not the first suspect in the formulation. By implementing three steps—ensuring moisture is trapped in the window, adjusting the scraper gap and angle, and incorporating the liner condition into routine inspections—most wall adhesion problems can be resolved. Formulation adjustments should be a last resort, not the first reaction.